Contact Kelly McNamara for information on products, services or locations.
Choosing High Quality Pipe Machine Equipment in 2026 requires more than comparing purchase prices. Production managers must examine forming accuracy, welding stability, energy consumption, automation, and after-sales support. A machine may look impressive on a showroom floor. Its real test appears beside a humming mill, where operators check wall thickness and diameter tolerance every hour.
Grand View Research reported that the global pipes market was valued at approximately USD 125 billion in 2023 and is expected to expand through 2030. This growth increases pressure on manufacturers to produce consistent pipes with fewer rejects. However, market expansion does not guarantee reliable equipment. Buyers should verify technical data through factory trials, independent inspections, and documented customer references. Useful checks include line speed under full load, thickness variation, motor temperature, changeover time, and spare-parts availability.
Quality expert W. Edwards Deming stated, “Quality comes not from inspection, but from the improvement of the production process.” His principle remains practical for pipe manufacturing. A strong machine should prevent defects, not merely reveal them later. ISO 9001 certification, CE conformity where applicable, and compliance with relevant ASTM, EN, or API requirements can support confidence, but certificates alone are not enough.
There is no perfect machine.
Some buyers still overvalue maximum output. That can be a mistake. A slower line with stable control may deliver better annual profit than a faster line producing irregular welds. This guide explains how to assess High Quality Pipe Machine Equipment using measurable performance, lifecycle cost, supplier credibility, and realistic production evidence.
High-quality pipe machine equipment in 2026 is defined by consistent performance, not a polished brochure. In real production, operators check wall thickness, roundness, weld quality, and surface finish throughout each shift. A reliable machine maintains stable temperature, pressure, and forming speed when raw material conditions change. That stability protects output and reduces expensive rework.
Modern controls also matter. Clear dashboards should show motor load, line speed, temperature trends, and alarm history. Useful sensors detect drift before a defect becomes visible. Automatic calibration can improve repeatability, but it cannot replace skilled inspection. The best systems support practical decisions rather than hide them behind complicated software. Data should be traceable, exportable, and protected from unauthorized changes.
Maintenance design reveals genuine quality. Accessible rollers, guarded drive parts, labeled wiring, and standard replacement components shorten service time. Energy use deserves attention too. Efficient motors and controlled heating can reduce operating costs without weakening production. Ask for documented testing, training records, spare-part availability, and measurable service response times. Talk to current operators when possible.
Small details matter.
However, no equipment remains perfect without disciplined operation. I have seen advanced lines lose accuracy because cleaning schedules were ignored. A strong supplier should explain limitations honestly, including setup sensitivity and expected wear. That transparency builds trust. It also helps buyers choose equipment that fits their materials, workforce, factory space, and long-term production goals.
The chart presents a practical 100-point procurement framework for evaluating pipe machine equipment in 2026. Dimensional accuracy and weld quality receive the highest weighting because they directly affect product consistency, leakage prevention, and compliance with applicable technical standards. Energy efficiency, safety compliance, production throughput, and maintainability help measure long-term operating value. The data represents evaluation weights rather than company or brand performance.
When selecting pipe machine equipment in 2026, performance should be measured, not assumed. In practical factory trials, I watch the line from coil loading to final cutting. Stable speed matters, but speed alone can hide defects. Check wall thickness, roundness, weld consistency, and cut length across several hours. A machine that runs fast for ten minutes proves little. Production leaves evidence.
Production capacity needs a clear calculation. Record actual output per hour, changeover time, scrap rate, downtime, and operator workload. Compare rated capacity with a supervised trial using your intended materials and sizes. If a machine claims six tons daily, ask about thickness, diameter, and shift pattern. Material changes can reduce output sharply. Include buffer time for tooling adjustments and maintenance. This is where many estimates become optimistic. I have seen schedules fail because loading delays were ignored. The spreadsheet looked perfect.
Assess performance through repeatability. Run multiple batches, inspect samples with calibrated gauges, and retain test records. Review motor load, temperature, vibration, and emergency-stop response during the trial. Ask for maintenance intervals, spare-part lead times, training scope, and documented acceptance criteria. Independent inspection can strengthen confidence, especially for high-volume lines. Still, no test removes every risk. Dust, inconsistent coils, and inexperienced operators may change results. Leave room for learning. A careful buyer values honest limitations as much as impressive numbers.
Selecting high-quality pipe machine equipment in 2026 requires more than checking production speed. Durability begins with the materials around forming, cutting, and heating zones. High-strength carbon steel frames resist vibration during continuous production. Stainless steel contact parts reduce corrosion from moisture, coolants, and cleaning chemicals. Good materials matter. However, “stainless” alone proves little. Its grade, thickness, and weld quality need verification through certificates and inspection records.
Critical rollers and dies should use hardened tool steel with stable surface treatment. This reduces scoring, dimensional drift, and replacement frequency. Copper alloy components can improve heat transfer in heating systems, but they still require hardness and electrical testing. Bearings should be sealed, correctly rated, and precisely aligned. Small gaps become costly failures. Request hardness reports, material certificates, weld inspection evidence, and factory acceptance test results. A practical inspection should include several hours of loaded operation, not just an attractive empty-run demonstration.
Manufacturing details show whether equipment was built for years or merely assembled for delivery. A rigid frame needs stress relief after welding, accurate machining, and accessible service points. Cable routes should remain protected from heat and moving parts. Guards must be secure, while emergency controls stay easy to reach. In my experience, clear maintenance access often saves more downtime than higher nominal speed. Still, no machine is perfect. Some suppliers provide strong materials but weak documentation. Others present polished records while overlooking alignment. Compare documents with physical checks, and record every deviation before acceptance.
| Equipment Area | Recommended Material | Important Material Properties | Manufacturing Features to Check | Applicable Standards or Tests | Durability Benefit | Practical Inspection Point | Overall Suitability |
|---|---|---|---|---|---|---|---|
| Main Machine Frame | Welded structural carbon steel, typically equivalent to common structural grades such as S355 | High yield strength, good weldability, and adequate stiffness for heavy loads | Stress-relieved welding, precision machining of mounting surfaces, diagonal bracing, and verified dimensional tolerances | EN 10025-2; weld quality inspection according to ISO 5817 | Reduces frame distortion, vibration, and alignment loss during continuous operation | Check weld continuity, flatness of mounting pads, frame squareness, and deformation after a loaded trial run | Very High |
| Roller Shafts and Drive Shafts | Quenched-and-tempered alloy steel, such as 42CrMo4-type steel | High tensile strength, fatigue resistance, and improved toughness after heat treatment | Controlled heat treatment, journal grinding, radiused shoulders, and non-destructive testing for cracks | EN 10083-3; ultrasonic or magnetic-particle inspection where appropriate | Improves resistance to bending fatigue, torsional stress, and repeated impact loading | Verify hardness records, shaft runout, surface finish, keyway quality, and concentricity | Very High |
| Forming and Sizing Rolls | Hardened alloy tool steel or wear-resistant bearing steel, selected according to pipe material and load | High surface hardness, compressive strength, dimensional stability, and wear resistance | Computer-controlled turning or grinding, polished forming surfaces, balanced rolls, and replaceable roll tooling | Dimensional inspection; hardness testing; surface roughness measurement | Maintains pipe geometry and reduces scoring, surface defects, and frequent roll replacement | Check roll profile accuracy, surface roughness, hardness uniformity, and axial alignment | Very High |
| Roll Surface Treatment | Chromium plating, nitriding, or other verified wear-resistant surface treatment | Improved hardness, lower friction, corrosion resistance, and resistance to adhesive wear | Controlled coating thickness, strong adhesion, uniform coverage, and edge protection against peeling | Coating thickness, adhesion, porosity, and surface roughness tests | Extends roll service intervals when processing abrasive, coated, or high-strength steel strip | Inspect for flaking, pitting, uneven coating, sharp edges, and changes in roll diameter | High |
| Bearings and Bearing Housings | Through-hardened bearing steel with machined cast or fabricated steel housings | High rolling-contact fatigue strength, dimensional accuracy, and resistance to contamination | Correct fits and clearances, sealed lubrication paths, rigid housings, and accessible maintenance points | ISO 281 for bearing life calculations; ISO 15243 for damage classification | Reduces overheating, shaft misalignment, vibration, and unplanned downtime | Check bearing temperature, vibration, lubrication condition, axial play, and housing rigidity | Very High |
| Guides, Bushings, and Sliding Parts | Hardened steel, bronze alloy, or engineered wear material selected for the lubrication system | Low friction, seizure resistance, dimensional stability, and compatibility with the working environment | Replaceable wear inserts, accurately finished sliding surfaces, lubrication grooves, and protected adjustment screws | Surface roughness and dimensional tolerance inspection; friction and wear testing when required | Maintains strip or tube alignment and limits backlash in repeated adjustment cycles | Look for uneven wear, scoring, excessive clearance, blocked lubrication passages, and difficult adjustment | High |
| Hydraulic Cylinders and Manifolds | Honed steel cylinder tubes, alloy-steel rods, and corrosion-resistant rod coatings | Pressure resistance, smooth bore finish, rod hardness, and seal compatibility | Honed bores, concentric rod machining, protected seals, clean hydraulic assembly, and pressure testing | ISO 4413 for hydraulic system safety; pressure and leakage testing | Prevents loss of forming force, oil leakage, unstable positioning, and contamination-related failures | Check rod surface, seal leakage, pressure holding, hose routing, and cleanliness of hydraulic oil | High |
| Electrical Control Cabinet | Powder-coated steel enclosure with copper conductors and industrial-grade insulation materials | Mechanical protection, heat resistance, electrical insulation, and resistance to dust and moisture | Separated power and signal wiring, adequate ventilation, labeled terminals, cable glands, and spare capacity | IEC 60204-1; enclosure protection commonly selected using IEC 60529 IP ratings | Reduces electrical faults caused by vibration, overheating, dust ingress, and loose connections | Verify enclosure rating, cabinet temperature, grounding continuity, terminal tightness, and cable labeling | High |
| Gears, Couplings, and Gearboxes | Case-hardened or through-hardened alloy steel for gears; flexible couplings with replaceable elements | High tooth contact strength, core toughness, fatigue resistance, and tolerance to misalignment | Gear tooth grinding, controlled backlash, accurate alignment, sealed lubrication, and vibration-balanced rotating parts | ISO 6336 for gear load capacity; ISO 20816 for machine vibration evaluation | Improves torque transmission reliability and limits noise, pitting, tooth breakage, and shock damage | Check oil condition, gear backlash, tooth contact pattern, coupling wear, and operating vibration | Very High |
| Fasteners and Adjustment Hardware | High-strength alloy-steel bolts and corrosion-protected adjustment components | High preload capacity, fatigue resistance, thread durability, and resistance to loosening | Controlled tightening torque, locking devices, clean threads, hardened washers, and accessible service points | ISO 898-1 for carbon and alloy steel fastener mechanical properties | Maintains machine alignment and prevents loosening under vibration and cyclic forming loads | Check bolt grade markings, torque records, thread damage, locking method, and signs of fretting | High |
| Coolant and Lubrication Circuit | Stainless steel or protected carbon-steel piping with seals compatible with the selected fluid | Corrosion resistance, pressure stability, chemical compatibility, and resistance to temperature changes | Filtered circulation, accessible drains, protected hoses, leak-tested joints, and monitored fluid level | ISO 4413 principles for hydraulic fluid power systems; manufacturer fluid compatibility tests | Limits corrosion, abrasive contamination, heat accumulation, and premature bearing or roll wear | Inspect filters, hoses, fittings, fluid cleanliness, leaks, flow rate, and return-line condition | High |
| Protective Guards and Covers | Powder-coated carbon steel or stainless steel in corrosive or wet environments | Impact resistance, corrosion protection, safe access control, and dimensional stability | Rounded edges, rigid hinges, captive fasteners, inspection windows, and interlocked access doors where required | ISO 14120 for machinery guards; ISO 13857 for safety distances | Protects operators and internal components from chips, coolant, dust, and accidental contact | Check guard rigidity, hinge condition, interlock operation, coating quality, and unobstructed visibility | High |
| Corrosion Protection System | Multi-layer coating system: prepared steel substrate, primer, and industrial topcoat | Adhesion, resistance to humidity, chemical exposure, abrasion, and ultraviolet degradation | Controlled surface preparation, documented coating thickness, sealed welds, and protected machined surfaces | ISO 12944 for protective paint systems; coating thickness and adhesion tests | Reduces rust-related dimensional changes, structural weakening, and maintenance costs | Inspect coating thickness, edge coverage, weld areas, drain points, blistering, and exposed bare metal | High |
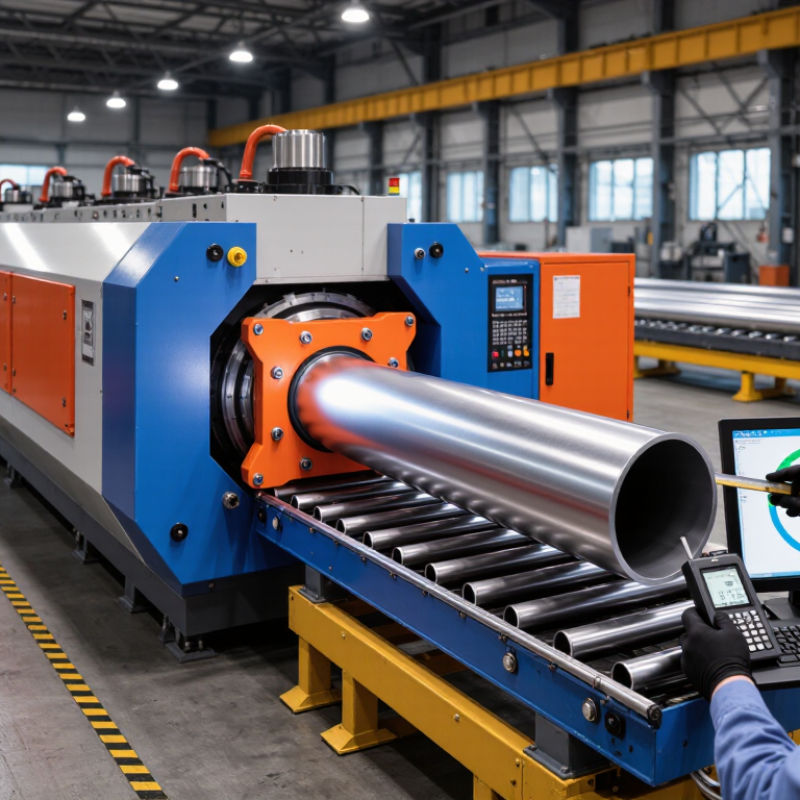
When choosing pipe machine equipment in 2026, compare measurable performance, not impressive brochures. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. Automation can improve repeatability, but it also adds sensors, software, and training demands. Check cycle time, reject rates, and operator access during a live trial. A fast line is not always a productive line.
Safety deserves equal weight. The International Labour Organization estimated 2.93 million work-related deaths globally in 2019. Ask for guarded forming zones, reliable interlocks, emergency stops, and clear maintenance isolation procedures. Test them physically. Do not accept screenshots as evidence. A useful audit records stopping distance, noise, heat, and the time required to clear a jam.
Energy and maintenance costs often decide the real purchase price. The U.S. Department of Energy reports that motor-driven systems consume more than half of industrial electricity in the United States. Request kWh per tonne, compressed-air demand, and standby consumption. Its Operations and Maintenance Best Practices Guide indicates energy savings of 5–20% may result from stronger maintenance practices. Compare bearing life, lubrication points, diagnostic alerts, spare-part availability, and remote support response times. No scorecard is perfect. A weakness remains: predicted savings can collapse when operators bypass alarms or maintenance records stay incomplete.
Choosing high-quality pipe machine equipment in 2026 starts with supplier evidence, not polished videos.
Request legal registration, factory details, production photos, test records, and customer references. Speak with at least two users who purchased similar equipment. Ask about output tolerance, breakdown response, and delivery delays.
Start with evidence.
A live video inspection can reveal wiring quality, guarding, calibration labels, and operator access. Verify every certificate with its issuing organization. Check the scope, expiry date, model coverage, and applicable safety requirements.
A certificate copy is not proof. Review the quality system, but inspect the machine itself. Neat documents cannot compensate for unstable welds or uneven forming.
Customization should match your pipe range, material grades, wall thickness, speed target, and floor layout.
Send drawings, samples, and utility limits. Request a trial using your material.
Test it live.
Measure roundness, surface marks, changeover time, noise, and scrap rate during acceptance. Put these results into the contract.
Clarify who pays for redesigned tooling, installation, training, software access, spare parts, and remote support.
Calculate total costs, including freight, duties, foundations, electricity, maintenance, consumables, and lost production during commissioning.
A low quotation may hide costly rollers or long service delays. I would keep a contingency budget. Even careful estimates miss something.
Have an independent engineer review the assumptions before payment milestones.